Injection moulding machine hydraulics run in unusual conditions: long high-pressure hold times, strongly cyclic motion and large oil temperature swings. The care priorities differ from ordinary hydraulic plant, and the two most common complaints are leaks and unstable hold pressure.
Unstable hold pressure shows straight up in the parts: sink marks, flash, dimensional variation. Diagnose in this order: read the pressure curve (modern machines all have one), then check the relief and proportional valves, and last the cylinder internal leakage.
Proportional valves are extremely sensitive to oil cleanliness. On a machine with drifting hold pressure, eight times in ten the proportional valve spool is slightly sticky or the oil is dirty. Checking the oil and cleaning the valve is far cheaper than replacing it — and usually works.
The accumulator is critical in the hold-pressure and fast-motion circuits. Wrong pre-charge shows as slow motion and large pressure swings. Measure the nitrogen pre-charge every six months.
The mould and process parameters also affect hold-pressure behaviour. If the machine checks out but the pressure is still unstable, work through it with the process people — do not keep circling inside the hydraulics.
 FIELD · SCHH-2026
Injection moulding machine leaks concentrate in a few places: the injection cylinder rod seal, the platen tie-bar area, the power-unit pipe joints, and the mounting faces of the proportional and directional valves. Going through them one by one beats blindly changing seals.
For a leaking rod seal, first check the rod for scoring and the guide bush for wear. Changing the seal on a damaged rod just leaks again in days. Light rod scoring can be dressed with an oilstone; severe damage needs re-chroming or a new rod.
Pipe-joint leaks usually come from installation strain or vibration loosening. A hard pipe fitted under strain (forced into alignment) puts continuous stress on the joint and leaks sooner or later. Refit without the strain, switching to hose or adding an adapter where needed.
For a leaking valve mounting face, check the O-ring for ageing, flattening or wrong size, and check the face flatness. Out-of-flat mounting faces leak even with a new seal.
 FIELD · SCHH-2026
The ideal oil temperature for an injection moulding machine is 40–55 °C. High oil temperature drops viscosity, increases internal leakage, ages the seals, and destabilises hold pressure. Machines exceeding 60 °C in summer need focused attention.
The main heat sources: relief losses (the pump still relieving at high pressure while idle), throttling losses, and internal leakage. A servo-pump or VFD retrofit greatly cuts idle relief losses, typically saving over 30% on power — the mainstream direction for injection moulding energy retrofits.
Falling cooler efficiency is a common cause of rising oil temperature. Water-cooled: check water flow and scaling. Air-cooled: check the fan and fins. Cleaning the cooler yearly is a necessary maintenance item.
Analyse the hydraulic oil on interval. Injection moulding machines run heavy loads and hot oil, so the oil ages faster than in general equipment — sample viscosity, acid number, water and cleanliness every six months.
The clamping unit is the most dangerous part of the machine. The safety-door interlock, the safety valve (mechanical clamp safety block) and the emergency-stop circuit must be proven effective at every service. A failed safety device here is unacceptable.
Check the tie bars for scoring and for even stretch. Uneven loading across the four tie bars tilts the platen, hurting part quality and mould life. Measuring tie-bar stress with strain gauges is the professional approach; day to day, look first for abnormal wear on the bar surfaces.
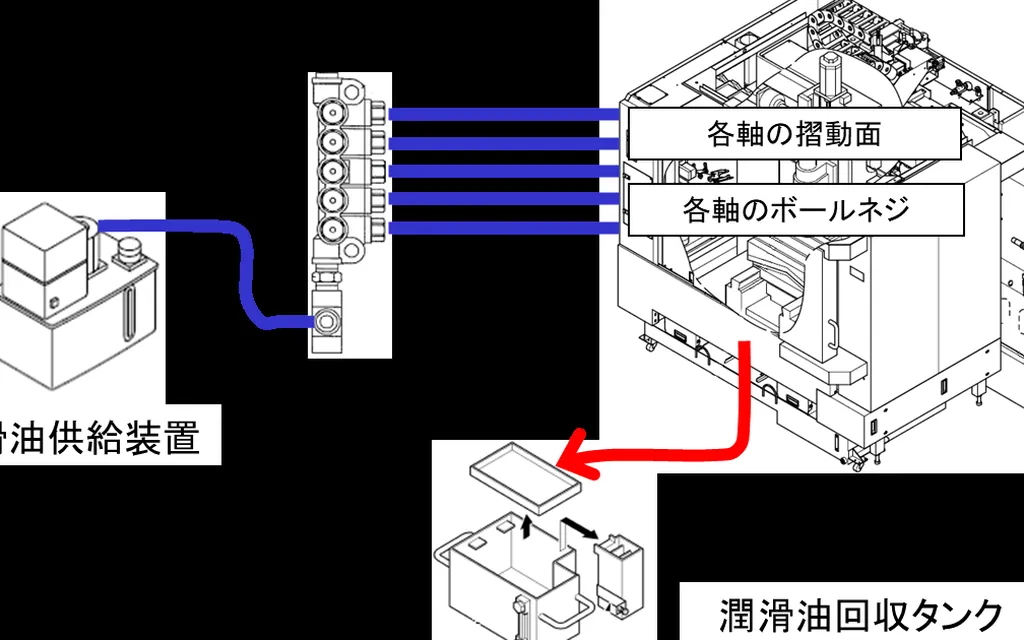
Confirm the central lubrication system delivers oil at every point, especially the moving-platen slide shoes, the mould-height adjuster and the ejection unit. Poor lubrication scores the guideways and is expensive to repair.
On dry-lubricated machines (wear-material slide shoes), check the clearance to the maker's requirement; adjust or replace the wear plates when it is out of tolerance.
| Maintenance item | Interval | Method | Acceptance criteria |
|---|---|---|---|
| Oil temperature record | Every shift | Panel readings | 40–55 °C, never above 60 °C |
| Hold-pressure curve check | Weekly | Compare with the machine's own curves | Stable pressure, no drift |
| Leak point patrol | Weekly | Visual: cylinders, joints, valve faces | No drips; log and fix any found |
| Safety interlock function check | Monthly | Safety door, e-stop, mechanical safety block | All operate reliably |
| Accumulator pre-charge pressure | Semi-annual | Dedicated charging tool | Matches the design value |
| Oil analysis | Semi-annual | Viscosity, acid number, water, cleanliness | Within in-service oil limits |
| Cooler cleaning | Annual | Descale water side / clean air-cooled fins | Heat transfer restored |
| Tie bar and clamping unit check | Semi-annual | Scoring, stretch, lubrication | Even loading, proper lubrication |
| Central lubrication point check | Monthly | Confirm oil at each point | Oil present at every point |
Injection molding machine hydraulics differ from general industrial hydraulics in three special features, and the maintenance plan must be designed around them. The first is the holding phase: after injection completes, the system must hold relatively stable pressure to guarantee part density and dimensions. Unstable holding directly causes part defects (sink marks, dimensional variation, internal stress), and its hydraulic root is usually internal leakage - leakage anywhere in the holding circuit's check valve, holding valve or cylinder seals means pressure will not hold. That is why testing holding performance (pressure decay rate during hold) is a dedicated item in injection molding hydraulic inspection.
The second is the strict requirement on oil temperature control: temperature swings on a molding machine directly change oil viscosity, which in turn affects motion speed and holding stability - so temperature control demands are stricter than for ordinary hydraulic equipment. Another trait is heavy heat load: the barrel heating zones are right there, ambient temperature is high, and with cyclic high-pressure work the oil easily runs hot. Cooling system checks (water or air), cooler cleaning and temperature control valve verification are mandatory before summer.
The third is cyclic impact loading: a molding machine's cycle is high-frequency (tens of seconds per cycle), and each cycle contains rapid clamping, injection, holding, mold opening and ejection stages, with pressure and flow changing violently. This duty affects component fatigue life far more than steady loading, which makes condition checks on accumulators, cushioning devices and shock suppression all the more important. Long-term hydraulic shock (water hammer) loosens pipe joints, damages seals and fatigues components; the countermeasures are adjusting shift speeds, adding shock-suppression circuits, and checking accumulator precharge pressure.
The oil change interval on an injection moulding machine is normally shorter than on general equipment, because oil temperatures are high and duty is intense. For mineral oil under normal duty we recommend testing oil condition every year and deciding on the result - most fall between 8,000 and 12,000 hours; harsh duty (a hot shop, continuous three-shift running, oil temperature chronically high) means a shorter interval. The criterion is not running hours but oil condition: viscosity change beyond the specified proportion, a clear rise in acid number, deteriorating cleanliness, excess water content - change the oil as soon as any one of them reaches its limit. Our advice is to send an oil sample for laboratory analysis at least once a year; that fee is far lower than the cost of replacing one hydraulic pump. When changing the oil, clean the tank, replace all elements and check cooler condition at the same time.
 FIELD · SCHH-2026
Judge case by case, starting with the scope and the pattern. If every movement is slow, look first at the shared hydraulic links: the pump's actual flow (measure with a flow meter and compare against the nameplate value to gauge volumetric efficiency), system pressure (does it reach the set value), oil viscosity (has it fallen because oil temperature is too high, or because the oil has degraded), and blocked elements (restricted suction starves the flow). If a single movement is slow, check the links specific to that movement: a sticking directional valve spool, throttle settings, internal leakage in that cylinder, or binding and poor lubrication in the mechanical parts. One factor is easily overlooked: oil temperature - when the machine runs too hot, viscosity drops and internal leakage rises, and the symptom is movements slowing after warm-up; measuring oil temperature confirms this at once. We recommend measuring three figures first - oil temperature, system pressure and movement time - and comparing them with normal values; the direction then becomes clear.
Injection moulding machines are among the biggest electricity consumers in a plant, and energy retrofits on their hydraulic systems usually pay back clearly. A conventional fixed-displacement machine works like this: within one cycle only part of the phases need high pressure and high flow, and in the rest the surplus energy is dumped through the relief valve as heat - that relief loss is the main source of waste. The mainstream retrofit is variable frequency drive: convert the fixed pump motor to an inverter-duty motor and adjust speed to the actual demand of each phase, eliminating relief loss; the saving depends on the process but is normally considerable. Going further, a servo pump package (a servo motor driving a fixed-displacement pump) responds faster, holds better accuracy and saves more energy, and is now the mainstream configuration on new machines.
The basis for the retrofit decision is the load curve: first record the pressure and flow demand of each phase, then calculate what share of energy goes over the relief valve - the larger the loss, the better the return. Machines with long cycles and a large share of holding time usually gain the most; short-cycle, fast-motion machines gain relatively less. This calculation needs measured data and cannot be estimated from the machine model - the first step of any energy project we take on is always measuring the data. Work out the numbers first, then decide whether to retrofit; never retrofit for the sake of retrofitting.
Beyond drive retrofits there are several low-cost energy and maintenance actions: restoring accumulator function (with correct pre-charge pressure it absorbs shock and assists supply, reducing pump load), improving cooling efficiency (oil temperature held in a reasonable band keeps viscosity stable, and stable viscosity means less internal leakage), leak control (internal and external leaks are both energy losses, so sealing leaks is saving energy), and optimising motion parameters (setting speeds and pressures to what the process actually needs rather than blindly high). These items need little investment, show results quickly, and suit a first step before any retrofit.
 FIELD · SCHH-2026
This article was written in-house by the Industrial Equipment Services Division. The thresholds, intervals and scrap criteria are field-experience values; in practice follow the equipment manufacturer's technical documents, current national standards and special-equipment safety regulations. Inspection and testing of special equipment (cranes, pressure vessels, etc.) must be carried out by a qualified body.
Send us your equipment list and operating conditions, and we will give you a workable inspection and maintenance standard.
 Scan to add Engineer Man on WeChat

 Guangzhou Yujihang Computer Technology Co., Ltd. · www.accpc.com.cn
 Guangzhou Henghuan Technology Co., Ltd. · www.hhrobotics.cn
 Nanchong Henghuan Robotics Co., Ltd. · www.hhrobots.cn