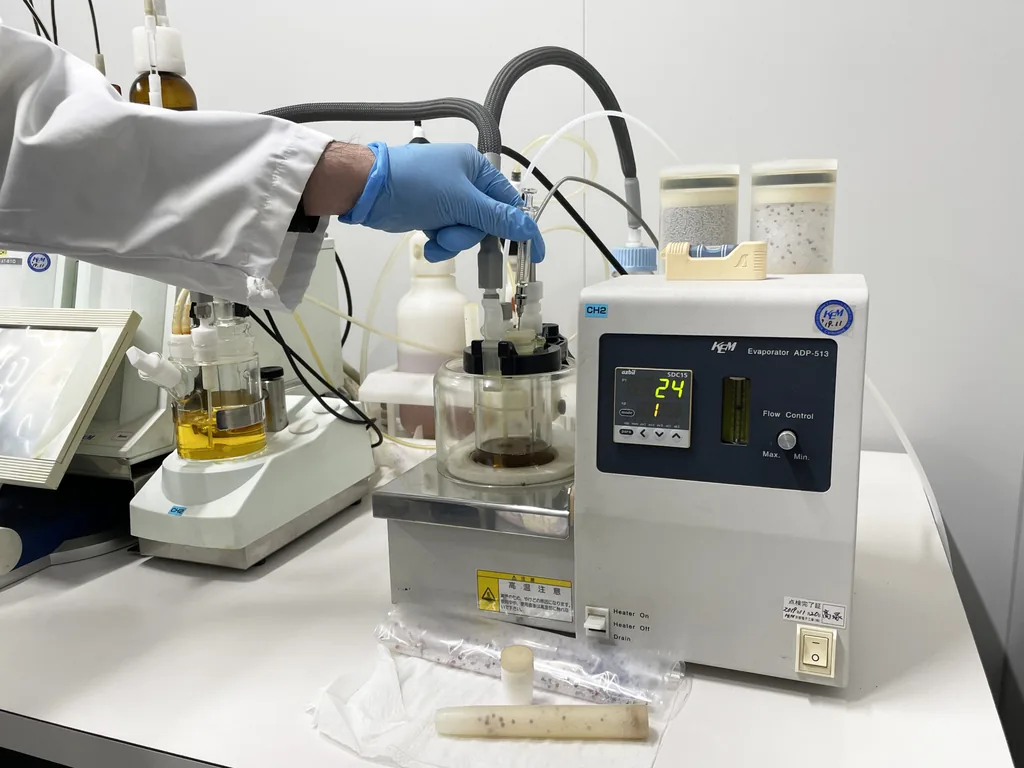
Eight families by machine type and industry. In each, we pick the most typical equipment and write up daily checks, periodic maintenance, scrap criteria and common mistakes as points you can follow directly on site.
 DAILY CHECK · SCHH-2026
The content comes from the front line of plant management and repair, and is written to be concrete: measurement methods, threshold values, interval suggestions and common mistakes — no empty talk.
All text in this section was written in-house by the Industrial Equipment Services Division. Thresholds and intervals are field-experience values; in practice follow the equipment manufacturer's technical documents and current national standards. For image-use notes and the disclaimer see Image Use & Disclaimer.
 FIELD · SCHH-2026
The material in this knowledge base looks scattered, but all of it falls into these three layers. Working out which layer you are missing is more useful than reading all thirty-odd articles.
We see these six again and again in different plants. Correcting them usually costs nothing - only a change of practice.
Over-greasing causes churning heat, a greater temperature rise, seals extruded and failed, and old grease carrying wear particles with no way out. Grease quantity is calculated from bearing type and speed, judged by old grease being purged or by the level mark. Too little grease burns a bearing out; too much burns it out just as surely, only more slowly.
A checklist without acceptance criteria only proves that someone signed it. The fix is to write every item as a decidable value or condition: temperature limit, oil level band, permissible clearance, a description of abnormal noise, degree of leakage. Only when the team can judge with it, record the judgement and compare records does inspection mean anything.
Replacing the failed part without investigating the cause means the same place keeps failing. Bearing wear can result from misalignment, improper lubrication, seal failure or a sudden load change. We do failure mode analysis and treat the causes along with the damage, aiming for one repair that lasts - and that is the dividing line between 'fixed and broken again' and 'fixed once, running for years'.
The manual gives recommended values for standard duty. A dusty shop versus a clean room, continuous versus intermittent running, the humid south versus the dry north - the sensible interval for the same machine can differ several times over. Correct the interval for the actual site conditions, then verify it with measured data; this is the most valuable step in any maintenance plan.
In dusty and damp environments, check the cooling airways and filters before the circuitry. Inverter failures, welded contactor contacts, drive over-temperature alarms - many of them root back to poor cooling and dust build-up. Heat is the silent killer: it raises no alarm, it just shortens component life year after year.
When the veteran leaves, the machine's history is cut off: what has been replaced, what parameters were adjusted, where the innate weak points are - nobody knows. One file per machine, a repair history, an accuracy baseline, lubrication cards: these paper records look like a chore, but they are the only way to turn individual experience into organisational capability.
 FIELD · SCHH-2026
If you have only one minute, remember the single most important point below for your equipment type. Full details are in the matching category.
 FIELD · SCHH-2026
We can build an executable inspection and maintenance standard around your equipment list and duty. One call: 18002209253.
 Scan to add Engineer Man on WeChat

 Guangzhou Yujihang Computer Technology Co., Ltd. · www.accpc.com.cn
 Guangzhou Henghuan Technology Co., Ltd. · www.hhrobotics.cn
 Nanchong Henghuan Robotics Co., Ltd. · www.hhrobots.cn