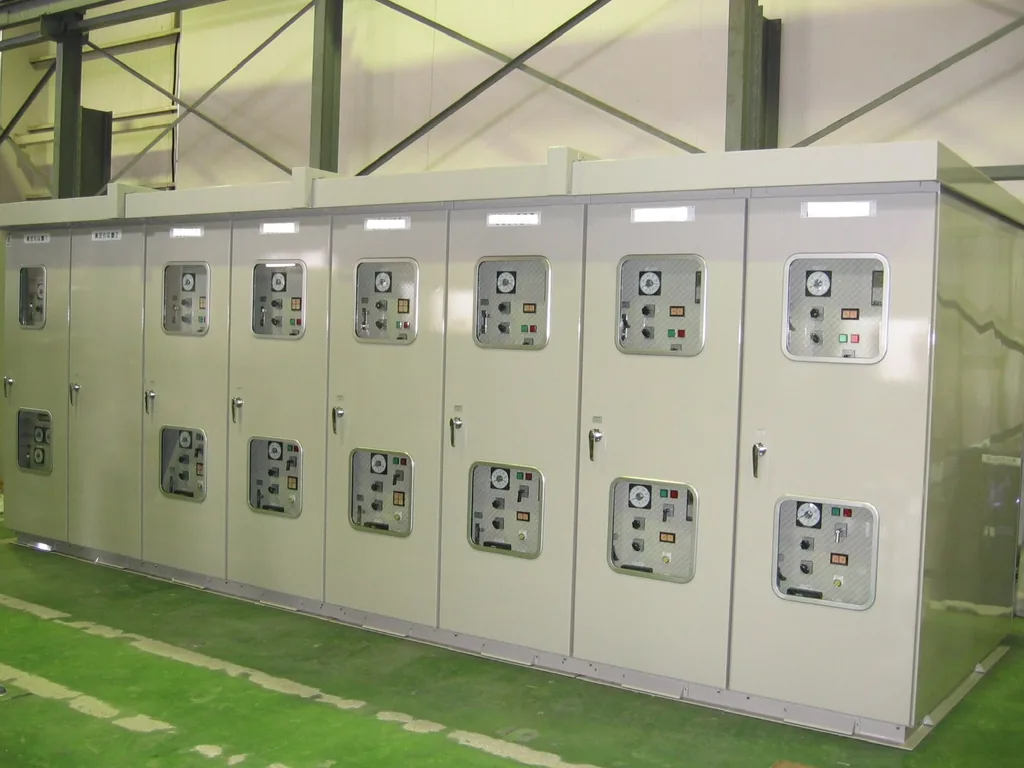
The most common stoppage on a machining centre is not an electrical fault — it is a blocked lubrication system nobody noticed. By the time the guideways are scored, the damage runs into tens of thousands of yuan. The five-fixed lubrication rule is not a slogan; it is a set of concrete parameters to be applied on every machine.
Fixed points: mark every lubrication point of each machine on a lubrication chart and stick it on the machine's flank. A machining centre typically has 15–30 points — linear guide blocks, ballscrew nuts, spindle bearings, the magazine cam box, the ATC mechanism. Miss one point and that spot becomes tomorrow's failure.
Fixed quality: VG68 way oil for the guideways (most models), VG32 or a dedicated grease for the ballscrew, and the manufacturer's spec for the spindle. Never substitute hydraulic oil for way oil — it lacks the anti-stick-slip EP additives, and low-speed feeds will stick-slip.
Fixed quantity: on centralised systems verify the output of every metering unit; on hand-oiled points write down exactly how many millilitres. Most lubrication failures are not missed oiling — they are over-oiling that overflows and wastes, or one metering branch blocked.
Fixed interval: grade by machine load. For two-shift heavy-duty machines check the oil level every 8 hours and metering output monthly; single-shift light duty can relax to weekly level checks and quarterly metering checks.
Fixed owner: who oils, who checks, who records — write it on the check sheet and sign it. An unsigned lubrication log is one nobody owns three months later.
 FIELD · SCHH-2026
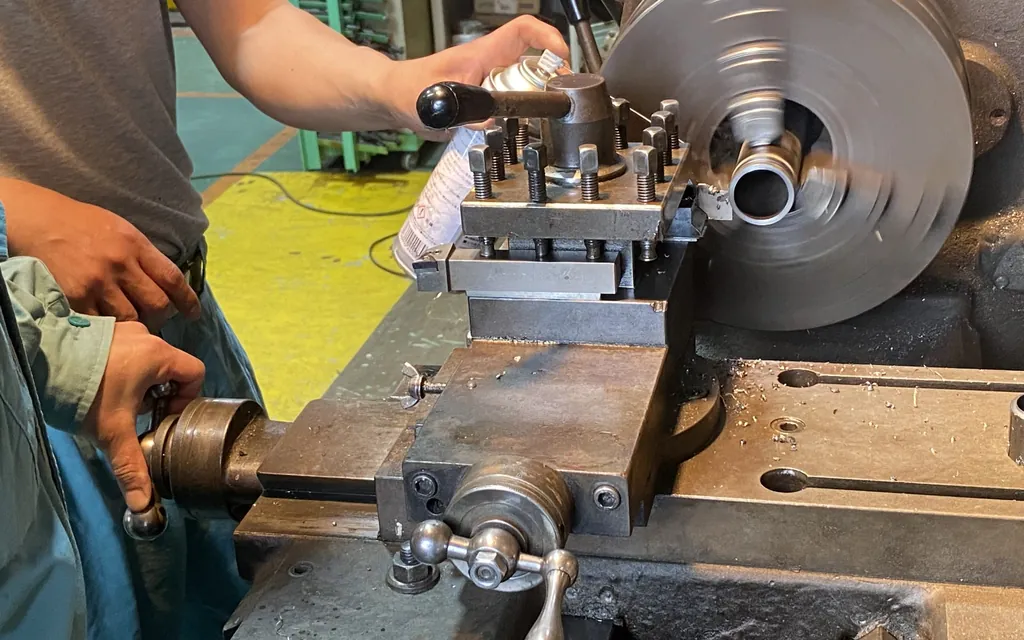
Linear guides fear two things: fine particles in the coolant, and knocks. Report a damaged cover (telescopic or bellows) within the same shift; leave it a week and the raceway collects a layer of grinding paste.
Push the covers by hand once a month to check for sticking and chip build-up. Keep the bellows drain holes clear; once blocked, coolant collects inside and the guideway sits soaked in it.
Measure ballscrew backlash every six months: set a dial indicator against the table, reverse 0.01 mm each way and read the lost motion. Above 0.02 mm, check nut preload and the support bearings. The same figure tells you whether the machine needs geometric accuracy restoration.
 FIELD · SCHH-2026
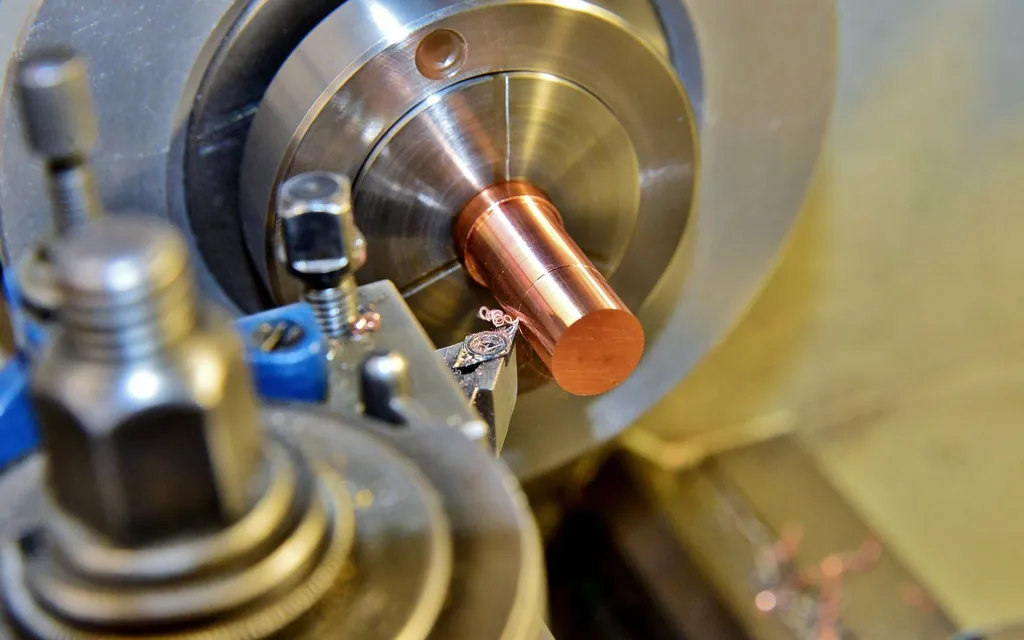
Degraded coolant destroys the oil film on the guideways. Check coolant concentration, pH and bacterial count monthly; top up with concentrate when it runs low, never plain water — diluting with water is a common mistake.
If lubricating oil gets into the coolant it emulsifies and fails. Check the oil tank for water ingress: draw a sample, let it stand and look for separation. Milky, emulsified oil must be changed in full and the tank cleaned — topping up with fresh oil is not enough.
| Maintenance item | Interval | Method | Acceptance criteria |
|---|---|---|---|
| Visual check of oil level and condition | Every shift | Tank level, oil colour | Level within the marks; oil clear, not emulsified |
| Metering unit output check | Monthly | Fresh oil weeping at every point | Oil present at every point |
| Cover and chip-clearance check | Weekly | Cover integrity, chip build-up | No damage, no sticking |
| Ballscrew backlash measurement | Semi-annual | Dial indicator, reversal lost motion | < 0.02mm |
| Coolant concentration and pH | Monthly | Refractometer, test strips | Concentration within the design range; pH 8.5–9.5 |
| Way-oil filter and tank cleaning | Annual | Replace the element, clean the tank | No sludge deposits |
Lubrication faults on machining centers share a trait: after a blockage the system does not alarm immediately - it first "cuts corners". One outlet of the divider stops delivering oil, a section of guideway runs dry, and weeks later the scoring shows up. So troubleshooting lubrication faults cannot stop at whether the pump is pumping: verify oil delivery point by point along the circuit - tank level and oil type, pump outlet pressure, the main line, each divider outlet, the oil film on the guideway - confirming section by section until the blockage reveals itself.
Once the blockage is found, push one step further back: why did it block? There are four common answers - wrong oil (incorrect grade, or mixed grades forming gum), filling without filtering (contaminants entering with the oil), intervals too long (oil oxidized and degraded), or water in the tank (coolant seepage causing emulsification). The blockage is the symptom; the management gap is the disease. Clear the blockage without fixing the management, and three months later the next divider blocks.
Solidify the findings into three artifacts: lubrication cards stating the oil type and interval for every point, an "oil-film visual confirmation" item added to the inspection card, and oil-change records kept on file and traceable. The maturity of lubrication management is judged by exactly these three: whether they exist, whether they are accurate, and whether anyone executes them.
A minor blockage, yes: remove that divider outlet, flush and clear it with clean oil, blow it dry, refit it, and confirm normal delivery in testing. But mind two things - first, check the other outlets of the same batch: when one blocks, the rest are usually close behind; second, check the oil type and oil condition: without removing the root cause, clearing the blockage only buys time. Dividers aged into internal leakage (inaccurate delivery volume) should simply be replaced - these parts are inexpensive, and replacing beats repairing.
 FIELD · SCHH-2026
The tank of a centralized lubrication system is normally changed once a year, or every six months under poor duty (heavy dust, high temperature, continuous running). Simple ways to judge oil condition: look at color and clarity (markedly darker or cloudy means degraded), let a sample stand and watch for a water line or separation (water ingress and emulsification), and rub it between the fingers for grittiness (contaminants over limit). Where possible, send a sample for acid number and viscosity analysis - the data is more reliable. When changing the oil, clean the tank and strainer too: residue of old oil accelerates the degradation of the new.
The "Five Fixed Rules" of lubrication - fixed point, fixed quality, fixed quantity, fixed schedule, fixed person - are textbook generalities. Brought down to a specific machine they must become checkable parameters, or they remain slogans. Fixed point: number and mark every lubrication point on every machine, with location maps for guideways, ball screws, bearings and chains, so a newcomer can find them from the map. Fixed quality: state the oil brand, grade and performance class for every point - no "close-enough oil will do". Fixed quantity: state the fill amount and the criterion for every point - sight-glass level for oil lubrication, grams or cavity fill ratio for grease. Fixed schedule: set the interval by duty and write it into the inspection card - not "periodically" but "every Wednesday, the first day of each month". Fixed person: assign a responsible person to every point, sign after execution, so any problem can be traced to the step.
Of the Five Fixed Rules, the one most often neglected is fixed quality. A considerable share of machining-center lubrication failures trace to oil mixing: guideway oil mixed with spindle oil, the same grade from different manufacturers mixed, or stock oil degraded past its shelf life. The anti-mixing measures are plain but effective - dedicated, labeled filling tools; oil drums stored in separate zones; and any grade change requiring a circuit flush with a record kept. Oil management looks like a housekeeping detail, but it is in fact an upstream variable of equipment life.
The fixed-schedule rule needs one companion mechanism: an oil consumption log. How much oil was added, when, and at which point - all recorded in the lubrication register. A sudden rise in consumption signals internal or external leakage; a sudden drop may mean a blocked oil line. Both trends surface faults early, and the whole cost of the record is one extra line written after each fill.
 FIELD · SCHH-2026
This article was written in-house by the Industrial Equipment Services Division. The thresholds, intervals and scrap criteria are field-experience values; in practice follow the equipment manufacturer's technical documents, current national standards and special-equipment safety regulations. Inspection and testing of special equipment (cranes, pressure vessels, etc.) must be carried out by a qualified body.
Send us your equipment list and operating conditions, and we will give you a workable inspection and maintenance standard.
 Scan to add Engineer Man on WeChat

 Guangzhou Yujihang Computer Technology Co., Ltd. · www.accpc.com.cn
 Guangzhou Henghuan Technology Co., Ltd. · www.hhrobotics.cn
 Nanchong Henghuan Robotics Co., Ltd. · www.hhrobots.cn